Ir para o conteúdo
Para um fabricante de alimentos de médio porte, a linha de embalagem certa não é automaticamente a opção mais rápida ou automatizada. É o sistema que pode lidar com seus produtos alimentícios e materiais de embalagem reais, produzir o número necessário de embalagens aceitáveis, apoiar sua mistura de SKU, se adequar ao seu regime de limpeza e permanecer prático para sua equipe operar e manter.
Resposta rápida: Comece com a restrição de produção que você precisa remover. Defina a comida, a embalagem acabada, a saída vendável necessária, a mistura de SKU, as trocas, o método de limpeza e as interfaces de fábrica antes de escolher o equipamento. Uma máquina automática autônoma ou uma célula modular podem ser um investimento melhor do que uma linha completa quando a demanda é variável, os formatos mudam com frequência ou o resto da fábrica não pode suportar a produção contínua.
A receita da empresa e a contagem de funcionários não definem o nível correto de automação. Dois fabricantes de alimentos de tamanho semelhante podem ter necessidades muito diferentes. Um pode executar dois produtos estáveis para longos turnos, enquanto outro produz dezenas de lotes curtos que exigem limpeza frequente de alérgenos e mudanças de embalagem. O primeiro pode se beneficiar de uma linha altamente integrada; O segundo pode criar mais valor com módulos flexíveis e tarefas manuais cuidadosamente retidas.
Este guia ajuda você a definir um limite de automação apropriado e transformá-lo em um requisito de fornecedor testável. Se você ainda estiver comparando famílias básicas de equipamentos, comece com o Guia do comprador de equipamentos de embalagem de alimentos.
Defina sua operação por complexidade de produção
“Médio porte” é uma linguagem de negócios útil, mas não é uma especificação de equipamento. Um fornecedor de linha de embalagem precisa de dados operacionais em vez de uma categoria da empresa. Comece com seis indicadores:
- Saída necessária: embalagens ou caixas aceitáveis por turno, não apenas a taxa máxima de ciclo da máquina.
- Complexidade SKU: o número de alimentos, porções, tamanhos de embalagens, filmes, bandejas, rótulos e formatos de caixas.
- Batch Padrão: Campanhas longas, tiragens curtas, picos sazonais ou lançamentos frequentes de produtos.
- Mudança e limpeza: mudanças de produtos, controles de alérgenos, mudanças de ferramentas e tempo de saneamento.
- Restrição de trabalho: onde a equipe, o trabalho repetitivo, o levantamento, a inconsistência ou o treinamento limitam a produção.
- Suporte técnico: os operadores, as competências de manutenção, a estratégia de peças sobressalentes e o tempo de resposta disponíveis após a instalação.
Use esses indicadores para descrever sua prontidão de automação. Não os force a uma pontuação universal. Uma planta pode estar pronta para automatizar a dosagem e a vedação, mas não está pronta para conectar todos os processos a montante e a jusante. Outra planta pode ter embalagens primárias estáveis, mas precisa de manuseio e paletização de casos porque a restrição de mão-de-obra está no final da linha.
Comece com a comida e o pacote acabado
Defina o alimento no momento em que ele entra no processo de embalagem. Um nome de produto por si só não é suficiente. Temperatura, umidade, óleo, partículas, poeira, viscosidade, fragilidade e variação normal de lote podem mudar a forma como o alimento é alimentado, porções, transferências e selos.
| Condição do produto | Perguntas para o documento |
|---|---|
| Pó ou partículas finas | Densidade aparente, poeira, aeração, ponte, estática e contaminação de vedação |
| Grânulos ou peças | Tamanho das partículas, quebra, segregação, orientação e comportamento de pesagem |
| Líquido ou pasta | Faixa de viscosidade, partículas, espuma, gotejamento e temperatura de preenchimento |
| Alimentos frescos, refrigerados ou congelados | Temperature, condensation, free liquid, handling damage and time outside controlled conditions |
| Fragile or irregular food | Drop height, compression, orientation, adhesion and acceptable damage |
The finished package must also be defined before you select the machine. State whether you need a rollstock bag, premade pouch, vacuum bag, tray, modified-atmosphere tray, skin pack, thermoformed pack, carton or bulk bag. Provide drawings or samples, material structures, dimensions, tolerances, seal surfaces, coding requirements and the tests used to accept a finished pack.
Use o food-characteristics and equipment matching guide to document difficult product conditions. Representative product and packaging samples should later be included in supplier trials; a successful empty-machine run does not prove product handling or package quality.
Mapeie todo o processo antes de escolher o equipamento
Draw the process from product supply to the shipping-ready case or pallet. Include every manual and automatic task:
Product supply → feeding or dosing → package forming or loading → filling → sealing → coding → inspection → case packing → case sealing → palletizing
For each step, record operator time, waiting, manual transfers, rejects, rework, replenishment, cleaning, changeovers and recurring stops. The purpose is to find the real production constraint. If sealing is slow and inconsistent, automating palletizing first will not increase the number of acceptable packages leaving the line. If a fast bagger repeatedly waits for product, buying a faster bagger can increase idle capacity without increasing output.
Also define the line boundary. “Fully automatic” may cover only forming, filling and sealing, while product loading, inspection, case packing or pallet handling remains outside the quotation. Ask every supplier to mark what enters the proposed system, what exits it and which tasks still require an operator.
Escolha um escopo de automação que se ajuste à restrição
You can normally consider four paths: a standalone automatic machine, an automated cell, a complete integrated line or phased automation. None is universally better.
| Automation path | Choose it when | Main risk to check |
|---|---|---|
| Standalone automatic machine | One operation is the clear constraint and manual loading or discharge remains practical. | The operator handoff or neighboring machine may become the next bottleneck. |
| Automated packaging cell | Several related operations should run together, such as dosing, bagging and sealing. | Interfaces with the retained manual or automatic processes must be defined. |
| Complete integrated line | Demand, products and packages are stable enough to justify coordinated continuous production. | Integration, recovery, maintenance and changeover complexity can offset the labor benefit. |
| Phased automation | The business is growing but demand, formats or capital timing remain uncertain. | Early equipment must include usable mechanical, electrical and control provisions for expansion. |
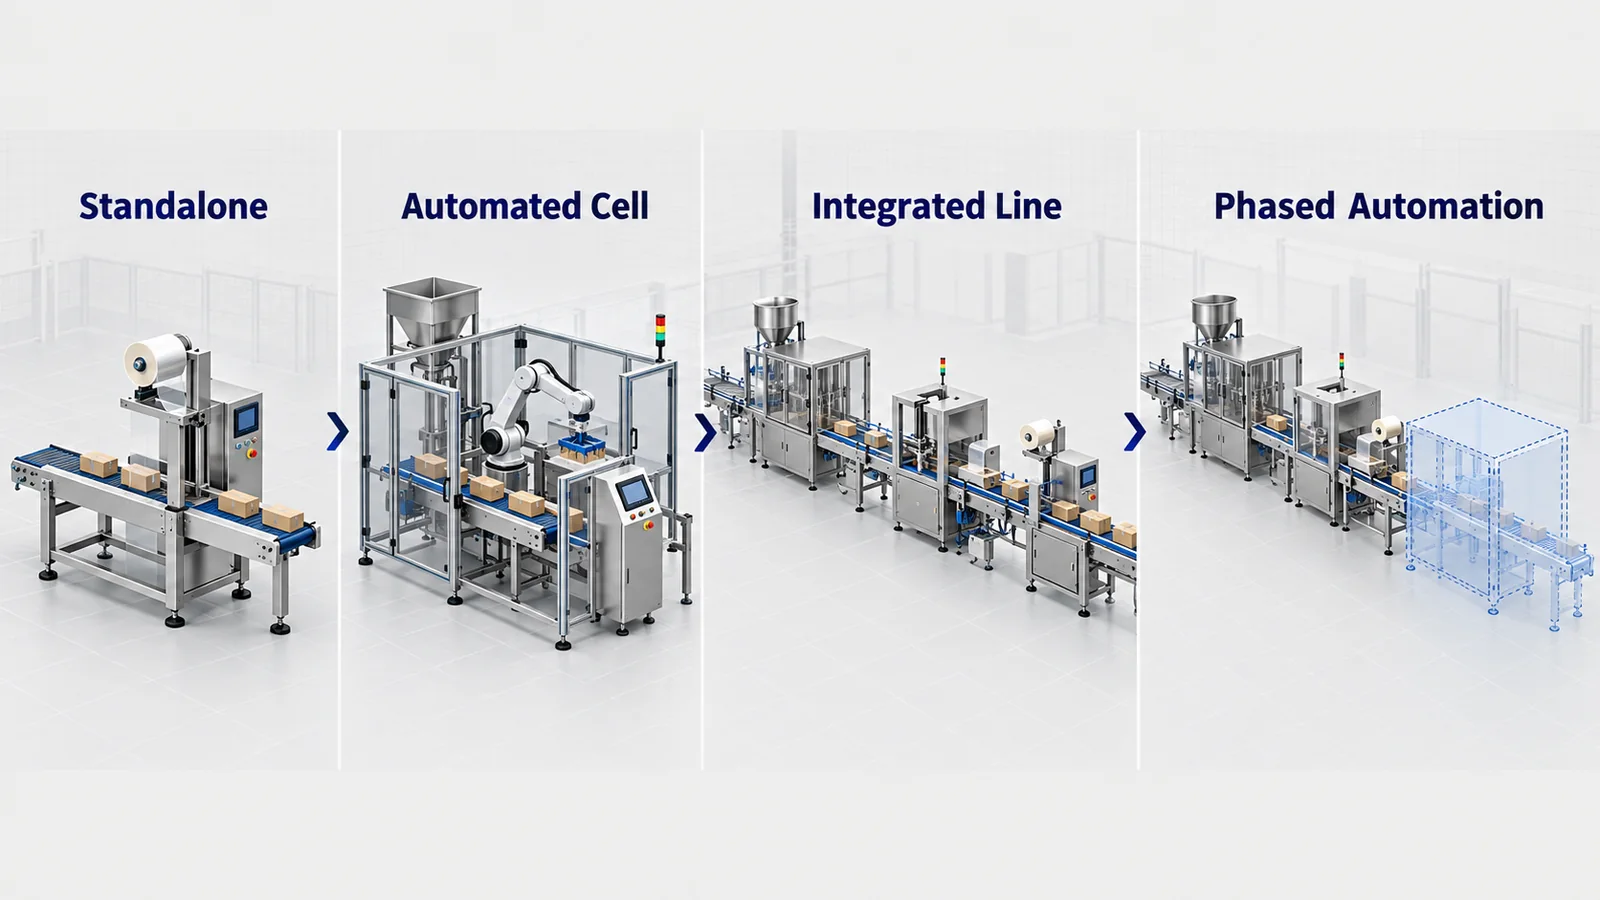
Phased automation is often practical for a mid-sized manufacturer, but only when the future line has been considered. Working heights, conveyor direction, controls, guarding, utilities and floor space can make later integration easy or expensive. Review HUALIAN’s packaging line solutions as examples of how equipment can be considered as part of a wider process rather than as isolated machines.
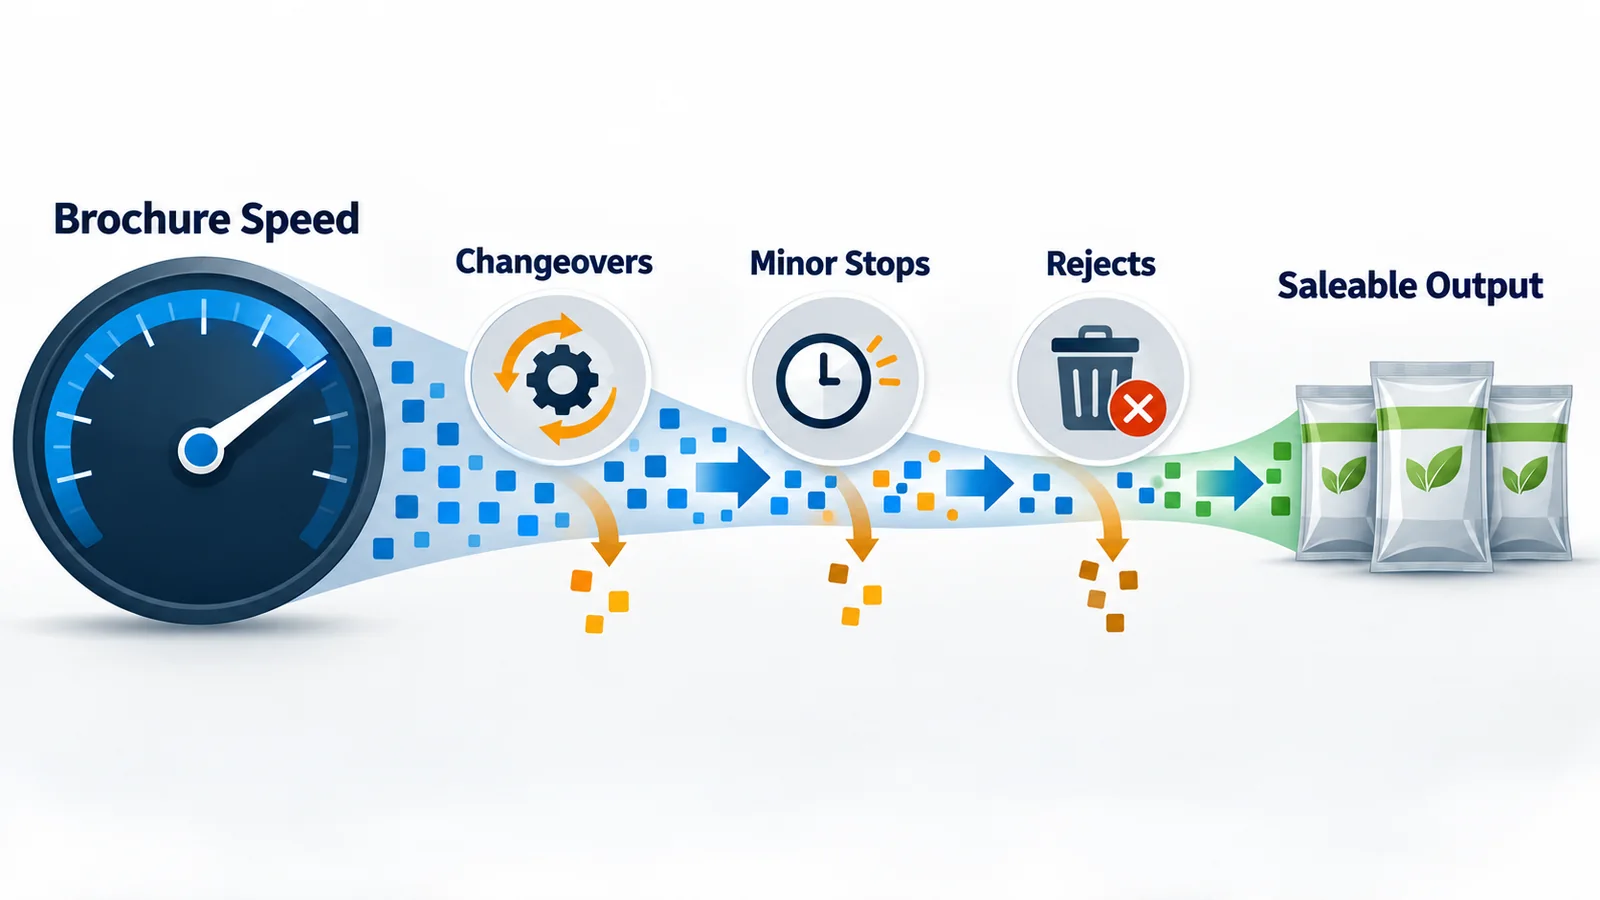
Especifique a saída vendável, não a velocidade da brochura
Machine speed is meaningful only when its basis is clear. A catalogue may show cycles per minute under defined conditions. Your business needs acceptable finished packs over an available shift. Product supply, manual loading, film changes, cleaning, changeovers, minor stops, rejects and downstream blocking all reduce the output you can sell.
Prepare the following information before requesting a proposal:
- Required acceptable packs or cases by SKU and shift
- Available production minutes after planned breaks and sanitation
- Batch size and number of changeovers
- Current and forecast demand
- Acceptable product giveaway, rejects and package defects
- Upstream supply rate and downstream handling capacity
- The definition and measurement method for an acceptable pack
Ask suppliers what product, material, staffing, test duration and intervention rules support their proposed rate. Use the food packaging machine capacity calculation to convert demand into a comparable requirement and identify the constrained stage.
Crie uma matriz de produto e pacote para cada SKU
A system that runs one ideal product does not prove that it can support your production schedule. Create a matrix for all launch SKUs and identify the difficult extremes: smallest and largest pack, lowest and highest fill, most fragile product, dustiest powder, most demanding film, deepest tray or product with the longest cleaning requirement.
For each product-package combination, record:
- Product condition and fill range
- Package dimensions and material
- Required tooling and change parts
- Stored recipe or manual settings
- Seal, code, label and inspection requirements
- Cleaning and cross-contact controls
- Expected batch length and target output
Then examine the changeover itself. Ask which guide rails, formers, molds, belts, nozzles, hoppers or recipes must change; which tasks require tools; how parts are identified and stored; and how the first acceptable pack is approved. A lower peak speed may be more productive when it enables faster, repeatable changeovers across short batches.
Higiene e limpeza como requisitos de produção
A stainless-steel exterior does not by itself prove that equipment is suitable for your cleaning task. Identify product-contact, splash and non-product zones. Review access, removable parts, joints, fasteners, hollow sections, cable routes, drainage and areas where food or cleaning liquid can collect.
Describe whether your process uses dry cleaning, wiping, foam cleaning or washdown, which chemicals are used and how often the machine must be disassembled. Frequent cleaning reduces available production time, so accessibility and restart checks affect both food-safety control and capacity.
In the United States, FDA requirements under 21 CFR 117.40 address equipment construction and cleanability for food operations; the exact requirements for your facility and market must be determined by qualified food-safety and engineering personnel. Review the FDA guidance referencing food-equipment CGMP requirements and use HUALIAN’s food packaging equipment hygienic-design checklist to structure a supplier review.
Planejar as interfaces de fábrica antes de congelar o layout
An automatic machine can perform well in isolation and still fail to deliver useful line output when transfers and interfaces are unstable. Record the product entry condition, pack orientation, working heights, conveyor speeds, required accumulation, reject route and response when an upstream or downstream machine stops.
Your layout should show:
- Available length, width and height
- Columns, doors, drains, walls and access routes
- Operator, cleaning and maintenance space
- Raw-material, packaging-material and finished-goods movement
- Electrical supply, compressed air, vacuum, gases, extraction, water and network access
- Line direction, working height and upstream or downstream connections
- Space and interfaces reserved for future equipment
When several suppliers are involved, assign ownership for mechanical interfaces, controls, safety zones, software signals and complete-line testing. If the line fails to reach the agreed output, the contract should make it possible to identify who records the issue, who leads diagnosis and how corrective work is verified.
Verifique se sua equipe pode suportar a automação
Automation can remove repetitive loading, sealing, handling or palletizing tasks, but it also changes the work. Operators may need to replenish materials, select recipes, perform quality checks, recover from alarms and verify changeovers. Maintenance teams may need to support sensors, drives, pneumatics, controls and connected-machine signals.
Ask each supplier to explain:
- The normal number and role of operators
- Daily, weekly and scheduled maintenance tasks
- Operator and maintenance training
- Alarm history, diagnostics and backup procedures
- Recommended critical and wear parts
- Remote and on-site support scope
- Expected response and spare-parts delivery arrangements for your location
Do not assume that “fully automatic” means unattended. Product and material replenishment, cleaning, quality release, format changes and technical intervention still need named owners.
Compare o custo total, não apenas o preço de compra
Build the business case from your current losses and the proposed operating model. Direct labor may be important, but it is only one input. Include product giveaway, packaging-material waste, rework, rejected packs, overtime, unplanned stops, cleaning, changeovers, injuries or ergonomic risks and outsourced packing where applicable.
The investment scope may include the main machine, tooling, conveyors, accumulation, inspection, coding, guarding, utilities, installation, commissioning, training, spare parts and planned production interruption. Operating costs may include labor, film or containers, energy, cleaning, maintenance, wear parts and downtime.
Count additional capacity as a financial benefit only when demand, upstream production and downstream logistics can use it. A faster packaging line does not create value if the food process cannot supply it or the market cannot absorb the extra output.
Transforme o requisito em propostas de fornecedores comparáveis
Send each shortlisted supplier the same controlled requirement. Avoid asking only for “an automatic food packaging line.” Use the food packaging machine RFQ checklist to document the product, package, output, formats, utilities, hygiene, services and acceptance basis.
Compare proposals using the same dimensions:
| Decision area | Evidence to request |
|---|---|
| Product and package fit | Trial plan and results using representative products and materials |
| Saleable output | Defined test duration, accepted packs, rejects, stops and operator interventions |
| Formats and changeover | Tooling list, change sequence, required tools and first-pack approval |
| Hygiene and cleaning | Zone review, materials, access, disassembly and cleaning procedure |
| Integração | Layout, interface schedule, signal list, line response and ownership |
| Segurança | Applicable design basis, risk assessment and agreed protective measures |
| Serviceability | Maintenance plan, parts list, diagnostics, training and service scope |
| Commercial scope | Included modules, exclusions, delivery basis, services and warranty terms |
Machinery safety should be addressed through a risk-based process appropriate to the supplied system and destination. ISO 12.100 (em inglês) describes general principles for machinery risk assessment and risk reduction; buyers and suppliers still need to determine the standards and legal requirements that apply to the actual project.
Validar a linha selecionada antes do envio
Agree the factory acceptance test before the purchase order or design freeze, not after the machine is complete. The protocol should state the machine configuration, products, packaging materials, formats, test duration, permitted interventions, required output, package-quality checks and handling of open items.
Measure acceptable finished packs rather than reporting only cycles. Test normal start and stop, agreed alarm and recovery conditions, reject handling, recipes, guards, changeovers and cleaning access. Record settings, stops, rejects and interventions so results can be reproduced.
Use o food packaging machine FAT checklist to build the protocol. Keep site-dependent utilities, final interfaces and operator performance in a separate site acceptance plan rather than treating the factory test as proof of every site condition.
Quando uma linha automática completa é a escolha errada
A complete line may be the wrong first investment when:
- Your food or package is still changing frequently.
- Demand is uncertain or strongly seasonal.
- You run many short batches with long cleaning requirements.
- One isolated operation is the dominant constraint.
- Upstream production cannot supply a stable flow.
- The factory lacks the maintenance resources to recover a connected line.
- Product and packaging materials have not been tested together.
- The financial case depends only on theoretical labor removal or peak speed.
In these conditions, choose a simpler machine, a modular cell or a phased plan when it can meet the required output with less integration risk. Preserve expansion options, but do not pay for complexity that your current products, demand and support structure cannot use.
Um processo de seleção prático de oito etapas
- Define the food and finished package. Include real operating variation and acceptance methods.
- Map the complete current process. Record labor, losses, cleaning, transfers and recurring stops.
- Identify the real constraint. Separate capacity, quality, labor, safety and traceability problems.
- Build the product-package matrix. Include all required formats and difficult extremes.
- Specify saleable output. Use acceptable packs under representative production conditions.
- Choose the automation boundary. Compare a machine, cell, complete line and phased plan.
- Compare equivalent proposals. Align scope, tooling, interfaces, services and lifecycle assumptions.
- Validate the solution. Agree trials, FAT, site checks and unresolved-item closure before commissioning.
Informações para preparar antes de solicitar uma proposta
- Food type, condition, temperature and handling risks
- Fill or portion range
- Package format, drawings, dimensions and material samples
- SKU list, batch sizes and change frequency
- Current and future acceptable output
- Cleaning method and cross-contact requirements
- Required coding, labeling, inspection and rejection
- Available layout and access route
- Electrical, air, vacuum, gas, water, extraction and network information
- Equipamentos Upstream e Downstream
- Operator and maintenance resources
- Required trial and acceptance criteria
Plan a right-sized food packaging line
Send your food details, package samples, SKU range, current output, target output and available floor plan. HUALIAN can review the information with you and discuss an appropriate equipment path and the tests needed before selection.
Perguntas frequentes
Qual é a melhor linha de embalagem para um fabricante de alimentos de médio porte?
There is no universal best line. The appropriate system depends on the food, finished package, saleable-output requirement, SKU mix, cleaning, factory interfaces, labor constraint and technical support available. Choose the simplest automation scope that can meet the written requirement with acceptable risk and room for planned growth.
Quando um fabricante de alimentos deve mudar de embalagens semiautomáticas para totalmente automáticas?
Consider greater automation when demand and product formats are stable, repeated manual tasks create a measurable constraint, upstream and downstream processes can support continuous flow, and the plant can operate and maintain the integrated equipment. Frequent changes, unstable demand or limited technical support may favor semi-automatic or modular equipment.
Você deve automatizar toda a linha de embalagem de uma só vez?
Not necessarily. Automate the dominant constraint first when one operation limits output or quality. A complete line is more appropriate when several connected operations must be coordinated and the complete production system is ready. If you automate in phases, define future interfaces before buying the first machine.
Como deve ser calculada a capacidade da linha de embalagem?
Calculate the acceptable finished packs required over available production time. Include cleaning, changeovers, minor stops, rejects, replenishment and upstream or downstream constraints. Ask suppliers to demonstrate sustained saleable output with representative products and materials rather than quoting only maximum cycles.
Uma linha de embalagem automática pode lidar com vários alimentos e tamanhos de embalagem?
It may handle a defined range, but every product-package combination creates requirements for feeding, tooling, recipes, sealing, inspection and cleaning. Build a matrix, identify the difficult extremes and test the contracted formats. Do not assume an untested combination is equivalent.
Como você compara duas cotações de linha de embalagem?
Use the same product and package matrix, output definition, line boundary, factory conditions and acceptance criteria. Compare included modules, tooling, interfaces, staffing, services, documentation, spare parts and lifecycle assumptions. A lower quotation may exclude essential equipment or integration work.
O que um teste de aceitação de fábrica de linha de embalagem deve provar?
It should verify the ordered scope, agreed formats, sustained acceptable output, package quality, controls, safety functions, fault recovery, changeover, cleaning access and documentation under a written protocol. Site utilities and final connected-machine performance may require separate site acceptance tests.
Conclusão
Choose an automated food packaging line from the operating requirement outward. Define your food and package, measure the real constraint, specify saleable output, account for SKU changes and cleaning, and decide which automation boundary your plant can support. Then compare suppliers using representative trials and measurable acceptance criteria.
For many mid-sized manufacturers, the strongest investment is not the most complex line. It is a right-sized system that produces acceptable packages consistently, can be maintained by the available team and can expand when demand and process stability justify the next stage.
Recursos relacionados
- How to Choose Food Packaging Equipment: A Practical Buyer’s Guide
- Como combinar as características dos alimentos com o equipamento de embalagem
- How to Calculate Food Packaging Machine Capacity
- Embalagem de Alimentos Máquina RFQ Checklist
- Equipamento de embalagem de alimentos Checklist de design higiênico
- Food Packaging Machine FAT Checklist