 コンテンツへスキップ

トラブルシューティングは、設定を変更する前に、まず人を保護し、証拠を保存し、製品、包装材料、機械、ユーティリティ、および統合の原因を分離する必要があります。.
クイック回答: 欠陥を定義し、影響を受けたパックを含み、現在のレシピと条件を記録し、何が変更されたのかを確認し、一度に1つのもっともらしい原因をテストします。アラームをクリアするだけでなく、持続的な実行と測定可能なパック結果で修正を確認します。.
この記事は コーヒー包装機械ガイド 1つの作戦決定に集中することで.
安全で繰り返し可能なトラブルシューティングシーケンスの使用
- 危険なエネルギーを隔離して、保護された場所や暖房された場所に入る。.
- 最後に確認された良好なチェック以降の製品を含む。.
- サンプル、時間、頻度、アラーム履歴、影響を受けるSKUで症状を説明します。.
- レコードコーヒー、バッグやフィルムのロット、レシピ、速度、温度、圧力、ガスおよびユーティリティ条件。.
- 製品、材料、オペレータ、清掃、メンテナンス、環境、上流または下流の機器など、何が変更されたかを尋ねます。.
- 製品、パッケージ、マシン、ユーティリティ、ラインインターフェイス仮説を分離する。.
- 承認された範囲内で1つの因子を変更し、合意されたサンプルで検証します。.
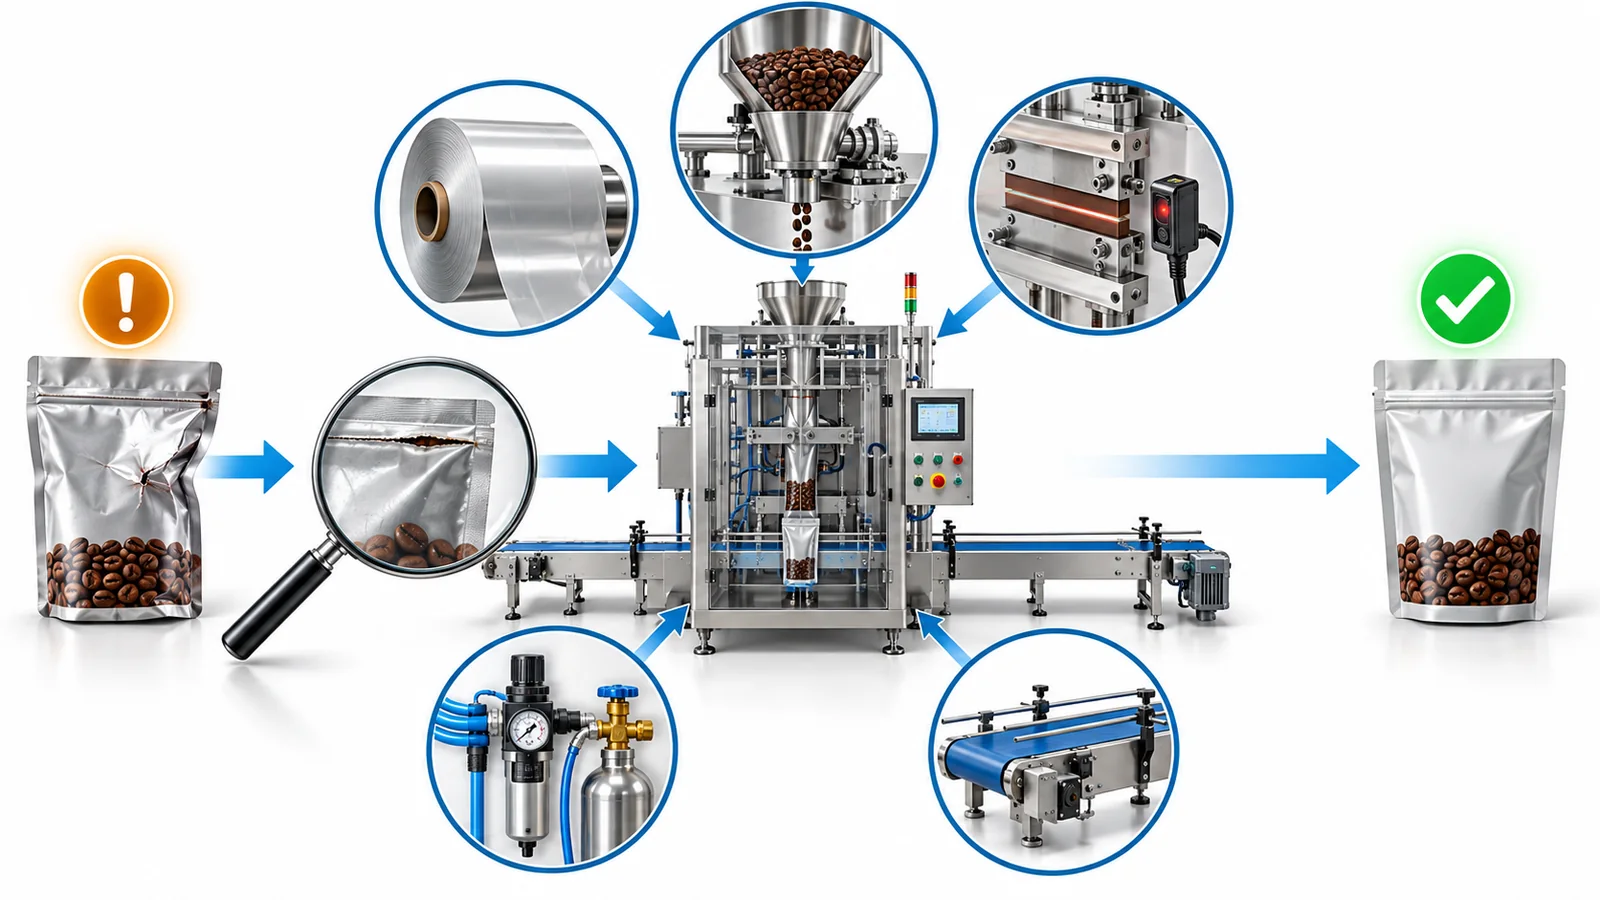
クイック症状—原因マトリックス
| 症状 | 最初のチェック | 共通原因ファミリー |
|---|---|---|
| 重量の変化またはドリフト | コーヒー密度/状態、ホッパーレベル、ビルドアップ、振動、校正チェック | 製品バリエーション、供給不安定性、投薬摩耗またはセットアップ |
| 弱いか漏出シール | コンタミネーション、フィルム/パウチロット、温度応答、圧力、ドウェル、アライメント | シールのコーヒー、間違った材料の窓、顎/バンドの状態 |
| ポーチが開きません | 袋の許容、雑誌、真空、グリッパーおよび静電気 | パッケージバリエーション、ピックアップ摩耗、タイミングまたは空気/真空供給 |
| フィルムトラックまたは登録移動 | ロールローディング、網道、張力、前の、スプライスおよびセンサー | 材料ロール、アライメント、張力または登録設定 |
| アザラシ区域の敷地 | カットオフ、シュート、セトリング、抽出、静的および速度 | 粉体挙動、充填経路、粉塵制御またはタイミング |
| 残留酸素不安定 | ガス供給、フロー、ノズル、タイミング、ヘッドスペース、シール、サンプル方法 | 供給、パージ形状、速度、漏れまたは測定 |
| 頻繁なショートストップ | 警報年表、センサーの汚染、蓄積および下流の状態 | 断続的な入力、マテリアルハンドリング、インターフェースまたは回復ロジック |
不正確な重量または過剰なプレゼント
全粒豆
豆のサイズ分布、断片、油性表面、ホッパーレベル、フィーダ振幅、計量ホッパー閉鎖、トラップされた豆、振動、承認された校正チェックをチェックしてください。ターゲットの平均値は依然として過剰な広がりを隠すことができます。.
挽いたコーヒー
粉砕、バルク密度、温度、空気入り、ホッパーヘッド、オーガーの蓄積、攪拌機の状態、カットオフおよび製品の沈降を確認します。プロセスが代わりに製品供給を安定させるかどうかを決定せずに、密度変化ごとに再校正しないでください。.
Verify with individual pack weights across a meaningful run. Record average, spread, underweights and giveaway.
弱いシール、チャネル漏れまたはしわ
Keep a failed package and mark its orientation. Check whether the defect repeats at the same jaw position, package side or time in the cycle. Inspect for coffee, folds, zipper or valve interference, material damage, uneven contact and unstable temperature.
Temperature, pressure and dwell work together within the package material’s sealing window. Raising temperature alone may distort material or hide contamination. After correction, inspect finished packs using the site’s defined seal and leak methods.
既製の袋の供給と開口問題
- Confirm pouch dimensions, mouth flatness, stiffness, friction, zipper and valve position against the approved sample.
- Load the magazine consistently and remove bent or blocked pouches.
- Inspect suction cups, vacuum level, filters, hoses, grippers and opening confirmation sensors.
- Check whether timing changed with machine speed or pouch size.
- Run approved samples from another lot to separate pouch variation from machine condition.
ロールストックの追跡、バッグの長さ、登録の問題
Confirm the roll is centered and correctly wound, the web follows the documented threading path, unwind tension is stable, the forming set is clean and correctly installed, and the registration sensor can see the mark. Inspect the splice and film edges.
Do not use an edge guide to compensate for a crooked roll, damaged film, contaminated roller or misaligned former. Verify bag length, print position, longitudinal seal and cross-seal alignment together.
コーヒー粉·シール汚染
First determine where powder escapes: feeder, auger outlet, filling chute, bag impact, withdrawal or sealing motion. Check extraction, static control, fill cutoff, bag opening, settling time and speed. A dirty jaw may be the result rather than the root cause.
Clean using the approved method and then correct the source. Evaluate seals after a sustained production run, not only the first clean packs.
不安定な窒素のフラッシング
Separate gas input from package result. Check supply capacity and pressure during demand, regulator and flow control, leaks, nozzle position, purge timing, package headspace, time to sealing and residual-oxygen analyzer method. Compare startup, steady production and restart conditions.
専用の使用 nitrogen flushing guide for coffee packaging to define the validation method. A high-purity supply does not prove low residual oxygen in the finished pack.
コーディング、検査、拒否欠陥
Check code consumables, mounting, trigger, product spacing and recipe. For inspection equipment, challenge the detection and reject sequence using the approved procedure. Verify that a rejected pack is positively removed and contained, and that downstream equipment cannot return it to saleable product.
繰り返しの停止とライン統合障害
Read the first alarm in the event sequence rather than the last cascade of alarms. Check ready/run/fault signals, sensor state, accumulation, starved and blocked conditions, upstream replenishment and downstream recovery. If the same short stop repeats, quantify frequency and lost time before changing logic.
について coffee packaging machine process explains how stations depend on each other.
リリース前に修正を確認
| 証拠 | Release question |
|---|---|
| サステイン·ラン | Did the line complete the agreed duration and SKU without recurrence? |
| Weight samples | Are average, spread, underweight and giveaway acceptable? |
| Package checks | Are seals, appearance, code, valve and contamination acceptable? |
| Atmosphere checks | Does residual oxygen meet the defined method where required? |
| 障害回復 | Does the line restart without duplicate fill, empty pack or lost traceability? |
| レコード | Were cause, action, setting, parts and verification documented? |
申請審査の準備
Hualianにあなたのコーヒータイプ、充填重量、パッケージ図面とサンプル、ターゲット販売可能な出力、SKUスケジュール、レイアウト、ユーティリティ、検査ニーズ、および現在の生産問題を送信してください。エンジニアリングチームは、一般的な構成に頼るのではなく、テスト可能な機械またはラインスコープを定義できます。.
よくある質問
なぜコーヒーバッグのシールが漏れるのか?
Common causes include coffee in the seal, folds, unsuitable material settings, uneven jaw contact, worn components or package features entering the seal.
走行中にパック重量が変わるのはなぜですか?
Coffee density and flow, hopper level, buildup, vibration, feeder behavior and dosing condition can all change the result.
なぜ既製のポーチが開かないのですか?
Check pouch tolerances and flatness, magazine loading, vacuum, suction cups, grippers, sensors, air supply and timing.
シールが弱いときはシール温度を上げるべきですか?
Not automatically. First inspect contamination, material, pressure, dwell, alignment and actual temperature response.
障害が修正されているかどうか?
Run representative production long enough to verify the measurable defect and confirm normal recovery, not just the absence of an alarm.








