콘텐츠로 건너뛰기

자동 소시지 포장 라인은 브로셔에서 가장 빠른 포장 기계를 중심으로 제품 흐름과 검증된 판매 가능한 출력을 중심으로 설계되어야 합니다. 라인은 가변 소시지 링크를 수신하고, 의도한 개수 또는 무게를 생성하고, 손상 없이 적재하고, 포장을 밀봉하고, 검사하고, 라벨을 부착하고, 병목 현상이나 위생 위험을 초래하지 않고 승인된 팩을 케이스로 옮겨야 합니다.
목차
비녀장라인 요구사항 사양으로 시작
제품군, 패키지 포맷, 정상 및 최대 수요, 공정 교대, 배치 크기, 필수 변경, 위생 창 및 예상 증가를 정의합니다. 필수 범위는 미래 옵션과 구분됩니다. 제품 프로세스를 소유하는 조직, 패키지 검증, 통합, 설치 및 수락을 통제하는 조직입니다.
각 SKU에 대해 문서 소시지 길이, 지름, 곡률, 중량 변화, 케이싱, 온도, 표면 수분 또는 오일, 링크가 연결되었는지 분리되었는지 여부, 압축에 대한 민감도 등이 있습니다. 이러한 변수는 자동 처리가 실제적인지 여부를 결정합니다.
전체 프로세스 흐름 매핑
- 요리, 냉각, 자르기 또는 연결에서 소시지를 받으십시오.
- 제품을 손상시키거나 시간 및 온도 제어를 손상시키지 않고 완충합니다.
- 필요한 수량을 분리하거나, 방향을 정하거나, 계산하거나, 무게를 재십시오.
- 가방, 열형 포켓 또는 트레이를 적재합니다.
- 공기를 제거하거나 대기를 교체한 다음 포장을 밀봉하십시오.
- 패키지를 검사하고 필요에 따라 코드, 무게 및 오염 물질을 확인합니다.
- 레이블 및 집계 팩을 케이스에 적용합니다.
- 부적합한 제품을 거부하고 추적성을 잃지 않습니다.
누적 점, 사람, 거부 경로, 청소 액세스, 유틸리티 및 유지 보수 여유를 사용하여 흐름을 그립니다.원시 제품 영역과 조리된 제품 영역에 물리적 또는 절차적 분리가 필요한지 확인합니다.
기본 패키지 플랫폼 선택
BAG-Based Vacuum Line 부근의 호텔
라인은 수동 또는 보조 가방 적재를 챔버, 벨트 또는 연속 진공 시스템과 결합할 수 있습니다. 불규칙하고 큰 포장에는 유연하지만 가방 열기 및 프리젠테이션은 자동화를 제한할 수 있습니다.
열포밍 선(Thermofforming Line)
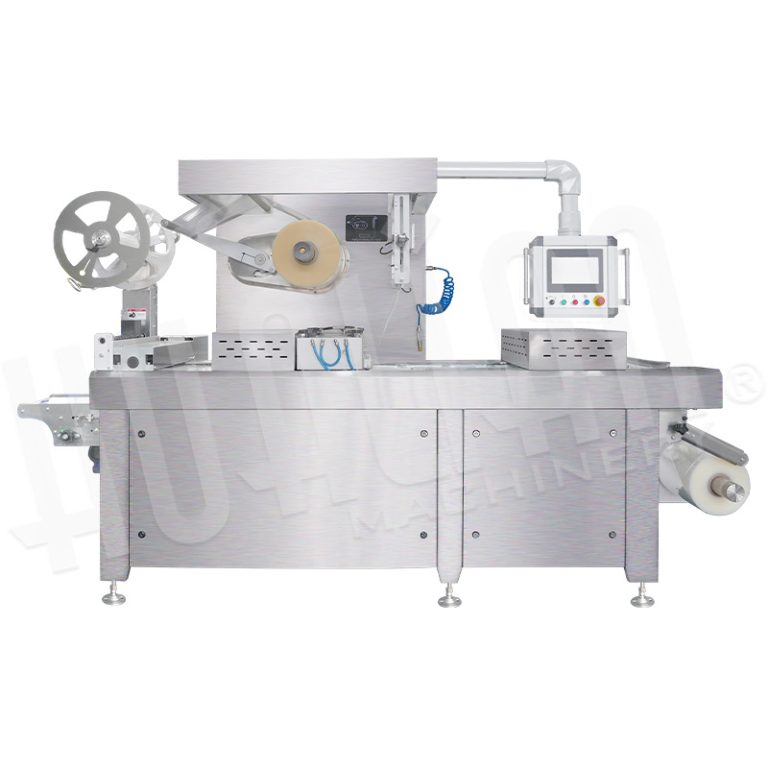
열포머는 롤스톡에서 인덱스 포켓을 생성하여 반복 가능한 팩과 연속 흐름을 위한 강력한 플랫폼입니다. 프로젝트는 캐비티 레이아웃, 로드 창, 필름 처리, 대피, 씰링, 절단, 레이블 지정 및 거부를 조정해야 합니다.
트레이 맵 라인
트레이 라인에는 덴스팅, 소시지 적재, 가스 교체, 씰링, 코딩, 검사 및 레이블 지정이 포함될 수 있습니다. 이 기능은 모양 및 소매 프레젠테이션에 중요한 경우에 유용합니다. 트레이 허용한도, 플랜지 청결, 헤드 공간, 가스 제어 및 라이딩 필름 호환성이 중심 설계 입력입니다.
에서 플랫폼 비교Compare the platforms in Thermofforming vs Chamber Packaging (열포밍 vs 챔버 패키징) 그리고 소세지용 진공 vs MAP 패키징.
엔지니어 제품 인피드 및 버퍼링
소시지가 이전 공정에서 벗어나는 방법을 정의합니다. 즉, 느슨하게 연결되어 있거나, 랙으로 연결되어 있거나, 계층화되어 있거나, 또는 벌크 컨테이너에 있습니다. 주입이 손상된 조각을 분리, 절단, 정렬, 카운트, 무게 측정 또는 거부해야 하는지 결정합니다. 제품 누적은 통제되지 않은 거주 시간이나 물리적 손상을 허용하지 않고 일시적인 중단을 흡수해야 합니다.
소프트 링크 또는 고정 링크의 경우 벨트, 가이드, 드롭 높이, 접촉 압력 및 청소를 테스트합니다. 자동 카운트 및 배치의 경우 전체 치수 및 모양 변형을 테스트합니다. 선택한 균일한 샘플을 기준으로 설계를 수행하지 마십시오.
로드 스테이션 설계
수동 로드는 워크스테이션에서 제품 및 빈 팩을 인체공학적으로 표시하고 패킹 머신 인덱스가 작업자 능력과 일치할 때 효율적입니다.레코드 도달, 반복, 제품 처리, 스태핑, 회전 및 회선 속도.
자동 로드에는 안정적인 들어오는 피치와 안정적인 탐지가 필요합니다. 누락, 이중, 곡선, 파손 또는 위치 이탈 소시지를 처리하는 방법을 정의하십시오. 중지, 중공이 비어 있는지, 포장을 거부하는지 또는 제품을 재순환하는지에 동의하십시오.
실제 용량 데이터를 사용하여 라인 균형 조정
기계적인 최대값이 아닌 양호한 출력을 사용하여 모든 모듈에 대한 용량 테이블을 만듭니다.
- 분당 일반 및 최대 수신 소시지
- 팩당 중량 또는 Pieces or weight per pack
- 기계 사이클당 팩 및 분당 사이클
- Good-Pack Rate 및 Planned Sampling 상세정보
- Labeler, 검사 및 케이스 패킹 능력
- 교체, 필름 또는 용지함 보충, 청소 및 고장 적용 범위
가장 느린 지속 모듈이 라인을 제어합니다. 정해진 짧은 정거장을 관리하기에 충분한 누적만 추가하십시오. 과도한 버퍼는 문제를 숨기고 위생 및 추적을 복잡하게 할 수 있습니다.
진공, 가스, 필름 및 씰 컨트롤 지정
운영자가 조정할 수 있는 배합식 변수 및 제어된 액세스가 필요한 변수를 식별합니다. 여기에는 진공 시간 또는 목표, 가스 배합식, 대피 및 플러시 순서, 밀봉 온도, 압력, 유입, 냉각, 형성 온도 및 색인 길이가 포함됩니다.
Vacuum and MAP are reduced-oxygen packaging processes. The FDA 식품 규정 makes clear that food-safety controls depend on the complete process. Define who validates the gas, atmosphere, shelf life, storage, and monitoring plan. Machine commissioning alone is not shelf-life validation.
검사 및 추적 가능성 추가
Define which checks are required and where they occur: product count or weight, metal detection or X-ray, seal or leak inspection, residual gas sampling, code verification, label presence and position, vision inspection, and case aggregation. Specify reject confirmation, reject-bin control, alarm escalation, and data retention.
Traceability should connect product lot, packaging-material lot, machine recipe, date and time, operator or batch, inspection results, and rejected quantity according to the site’s quality system.
계획 통제 통합 및 안전
Agree on line control ownership, start/stop sequence, starvation and blockage signals, emergency-stop zones, safe access, restart logic, recipe transfer, production reporting, remote access, cybersecurity requirements, and software backup. A mechanically connected line is not an integrated line until fault and recovery behavior is defined.
청소, 변경 및 유지보수를 위한 설계
Confirm cleaning boundaries, product-zone access, drainage, removable parts, approved chemicals, lockout procedures, and time needed to release the line after sanitation. Prevent cleaned and unclean components from crossing during tool handling.
List every change part by SKU and provide identification, carts, lifting aids, storage, and inspection. Simulate a complete product and package change during acceptance, including recipe selection and first-good-pack approval.
유틸리티 및 레이아웃 정의
Document electrical supply, compressed air pressure and quality, cooling-water temperature and flow, vacuum system, gas type and pressure, exhaust, drainage, network, ambient conditions, and washdown exposure. Measure available capacity while the rest of the plant is operating.
The layout must include access for film and tray replenishment, tool changes, pump service, electrical cabinets, cleaning, operator escape, and material movement. Check delivery route, door openings, lifting points, and final ceiling height before freezing the design.
단계 게이트 프로젝트 계획 작성
- User requirements: approve products, packs, outputs, standards, data, and acceptance criteria.
- Concept: compare packaging platforms, loading options, layouts, and ownership cost.
- Detailed design: freeze samples, interfaces, utilities, controls, safety, and documentation.
- Supplier trial: prove the difficult products and automation assumptions.
- FAT: test build quality, functions, recipes, faults, changeover, and representative production.
- Installation and SAT: verify the line in the actual factory with site utilities and operators.
- Ramp-up: track good output, labor, rejects, downtime, sanitation, and corrective actions.
자동 라인 견적 요청 체크리스트
- SKU matrix with product and pack samples
- Normal, peak, and future output by SKU
- Incoming product condition and upstream interface
- Required counting, weighing, orientation, and loading
- Packaging method, materials, atmosphere, and seal criteria
- Inspection, coding, labeling, rejection, and traceability
- Case format and end-of-line scope
- Changeover and sanitation targets
- Layout, utilities, environmental and safety requirements
- Documentation, trials, FAT, SAT, training, spares, and support
자주 묻는 질문
일반적으로 자동화하기 가장 어려운 부분은 무엇입니까?
Product separation, orientation, counting, and gentle loading are often harder than the sealing cycle because sausage shape and surface condition vary.
한 라인에는 얼마나 많은 버퍼가 있어야합니까?
Enough to absorb defined short interruptions without compromising product control. Size it from measured stop patterns and residence limits, not a generic rule.
한 공급자가 전체 라인을 소유해야합니까?
Either one integrator or several suppliers can work, but responsibility for interfaces, controls, safety, acceptance, and performance must be explicit.
Hualian can review thermoforming, vacuum, and tray-sealing line concepts. Submit a product and SKU matrix, package samples, target output, layout, utilities, and inspection scope to begin a defensible line design.